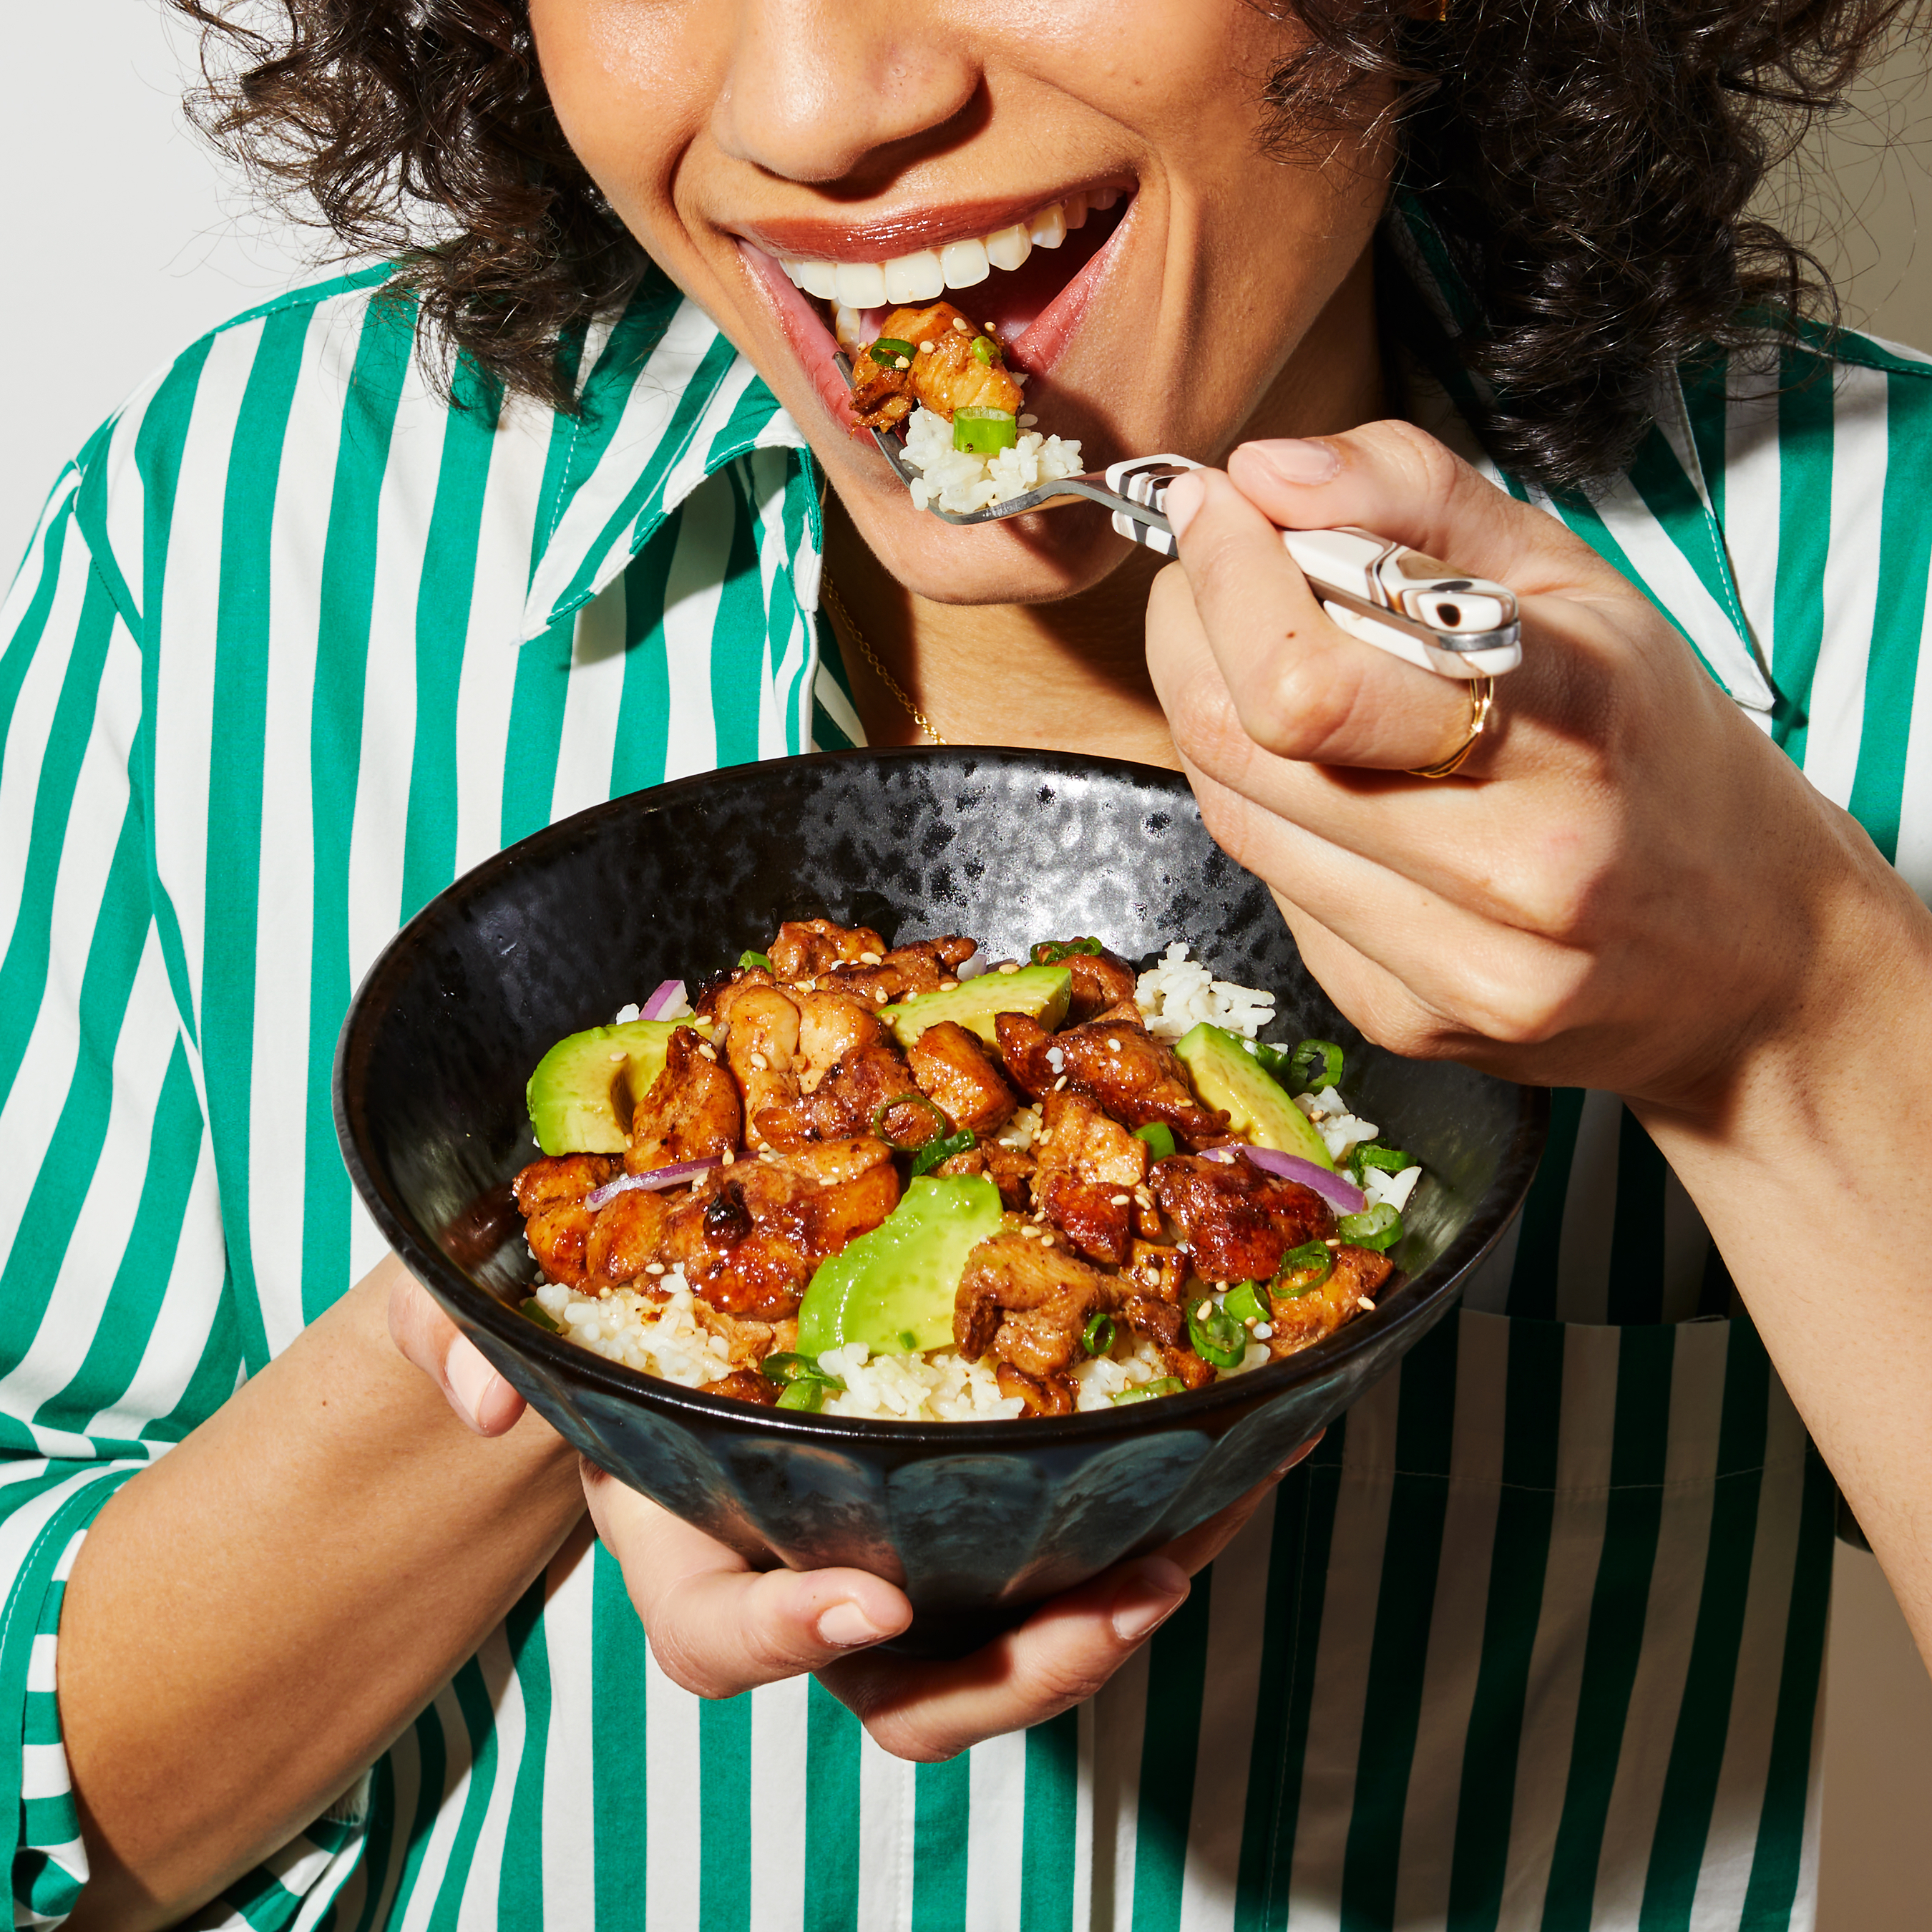
Holly Poultry has opened an 80,000-square-foot production facility in Anne Arundel County, Maryland, marking the company's first dedicated retail manufacturing operation after more than 30 years serving the foodservice channel. The plant is designed to support the company's branded lines — Easy Street and One Fine Chicken — along with an expanding roster of private-label partnerships.
Why the Facility Matters
For foodservice equipment specifiers and cold-chain operators, the build-out signals how regional poultry processors are investing in purpose-built prep-and-storage infrastructure to meet the distinct throughput and SKU-management demands of retail versus foodservice. Retail fresh poultry requires rapid changeovers between seasoning profiles, tight date-coding windows, and chilled staging capacity that differs substantially from bulk foodservice pack lines. Holly Poultry's decision to construct a standalone retail facility — rather than retrofit existing foodservice space — reflects an industry-wide recognition that mixed-use processing environments create bottlenecks when consumer-pack velocity scales.
Zach Fine, CEO of Holly Poultry, framed the investment in terms of capacity headroom: "This facility is a major investment in that opportunity. It gives us the capacity to serve the customers choosing our products today while creating room to expand into new retailers, build new private-label partnerships and keep pushing what fresh poultry can be."
Capacity and Channel Reach
The new Anne Arundel County operation is projected to create 140 net new jobs and gives Holly Poultry room to accelerate retail distribution beyond its current footprint. Easy Street — the company's pre-diced, dry-seasoned No Antibiotics Ever chicken thigh line — is already placed at Giant Food, The Giant Company, Harris Teeter, ShopRite, Shaw's, and Hannaford. At top-performing retailers, the brand is averaging more than 30 units per store per week across a three- to four-flavor set, which implies meaningful production throughput requirements at scale. Flavors include Korean BBQ, Street Taco, Peruvian, Shawarma, and Chili Crisp, each moving from refrigerated case to plate in approximately seven minutes.
One Fine Chicken, the company's value-positioned No Antibiotics Ever line priced below traditional national brands, occupies the everyday poultry aisle and adds a second SKU family the new facility will support. Private-label production — developing and manufacturing fresh poultry under retail partners' own brands — rounds out the plant's workload and is often the highest-volume, most specification-sensitive segment of a processor's retail business.
Cold Chain and Build-Out Context
Regional processors expanding into retail face a capital-intensive transition: retail-ready fresh poultry demands precise temperature-controlled environments throughout receiving, processing, packaging, and finished-goods staging. The 80,000-square-foot footprint puts the Anne Arundel facility in the mid-tier range for dedicated fresh-protein retail plants, large enough to support multi-SKU runs but compact enough to maintain the cold-chain integrity that perishable date-coded products require. Operators and equipment consultants working in refrigeration and cold storage will recognize the profile: purpose-built retail protein plants of this scale typically require multi-zone refrigeration, controlled-atmosphere staging areas, and high-throughput wrapping and labeling lines.
Amy Gowan, president and CEO of the Anne Arundel Economic Development Corporation, noted the investment "strengthens our local manufacturing economy, creates meaningful job opportunities and reinforces the region's role in the continued growth of Maryland's food industry."
Holly Poultry's transition from a primarily foodservice supplier to a dual-channel processor with a dedicated retail plant mirrors moves being made across the fresh protein category, as processors seek to capture margin and velocity by owning more of the consumer-facing supply chain. For the equipment trade, projects of this type generate sustained demand for refrigeration, prep and portioning, modified-atmosphere packaging, and cold-staging systems — making the Holly Poultry expansion a project worth tracking as it ramps production.
Written by Michael Politz, Author of Guide to Restaurant Success: The Proven Process for Starting Any Restaurant Business From Scratch to Success (ISBN: 978-1-119-66896-1), Founder of Food & Beverage Magazine, the leading online magazine and resource in the industry. Designer of the Bluetooth logo and recognized in Entrepreneur Magazine's "Top 40 Under 40" for founding American Wholesale Floral, Politz is also the Co-founder of the Proof Awards and the CPG Awards and a partner in numerous consumer brands across the food and beverage sector.